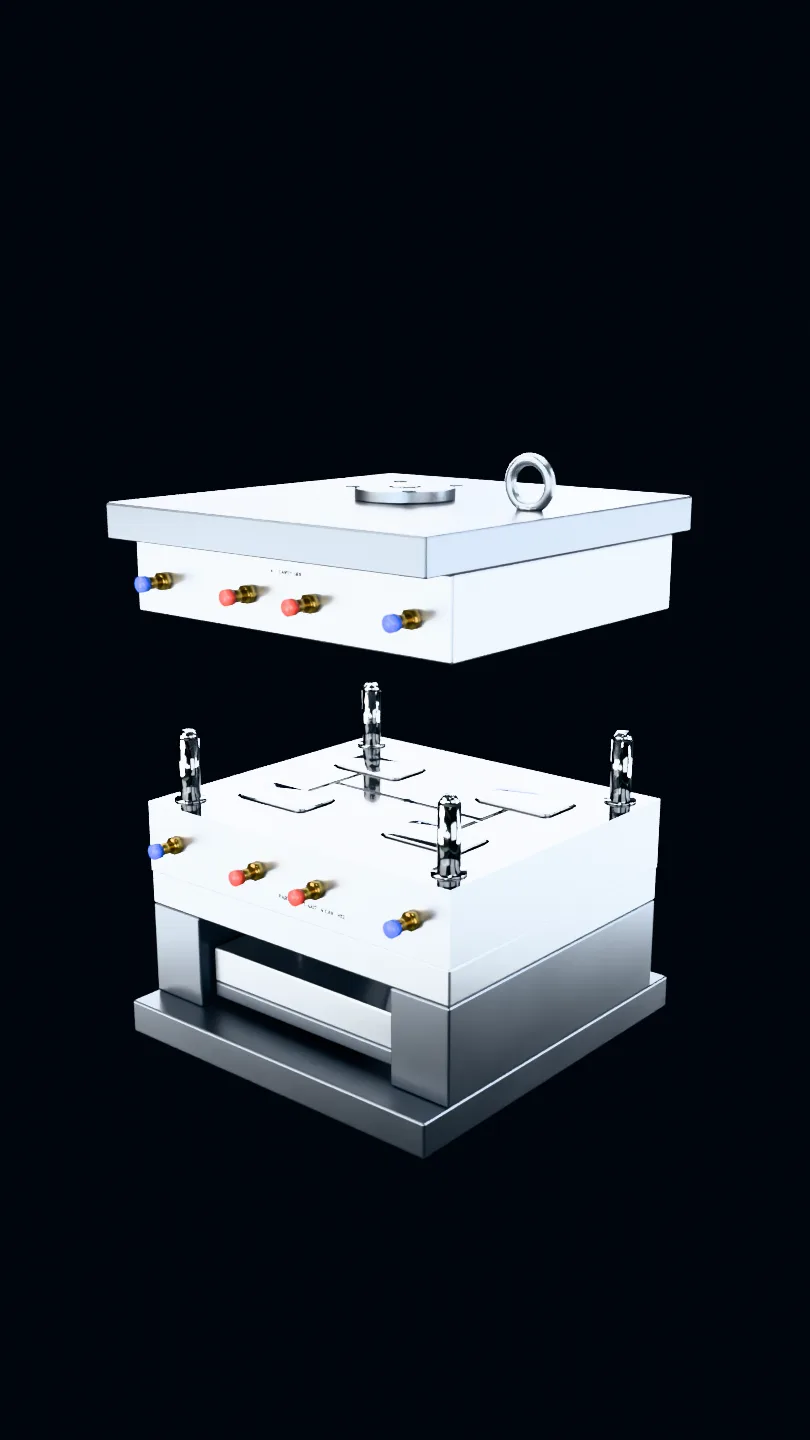
Custom plastic injection molding

One mold.
Millions of
identical parts.

We check your design, build the mold in our own tool room and run your production. Part one and part one million measure the same.

  • ISO 9001
  • ISO 13485
  • IATF 16949
  • Engineers answer in 2 days
  1. 01 / 05

    Clamp

    The two halves of the mold lock shut under 220 tons of force.

  2. 02 / 05

    Inject

    Melted plastic fills all four cavities in under two seconds. Where it enters, the gate, decides how it flows.

    How we choose gates
  3. 03 / 05

    Cool

    Water channels in the steel set the shape. This is where warping is won or lost.

    Stop parts warping
  4. 04 / 05

    Open

    The mold opens along the parting line. The parts stay on the core side, ready to come out.

  5. 05 / 05

    Eject

    Pins push the parts free, and the next cycle starts. Here: four parts every 28 seconds.

    See parts we make
  6. That was one cycle

    We repeat it until your order is done.

    And we measure the parts the whole way through.

Scroll to run a cycle
01How a project runs

Two parts to every project.

First we build your mold. Then we use it to make your parts, for as long as you need them.

1

The mold

Once · 6–10 weeks · you own it

  1. Design reviewWeek 0
  2. MaterialWeek 1
  3. Mold designWeek 1–2
  4. Mold buildWeek 2–8
  5. First samplesWeek 8
  6. Your approvalWeek 9
  • You own the moldIt's written into your quote.
  • We maintain it freeCleaned every run, serviced by shot count.
  • Stored here, readyReorders skip setup and ship fast.
2

The parts

Every order · reorders ship in 2–3 weeks

  1. Mold
  2. Inspect
  3. Assemble
  4. Ship
1orders run

03Parts we make

Parts we mold every day.

01 / 07 Drag or scroll

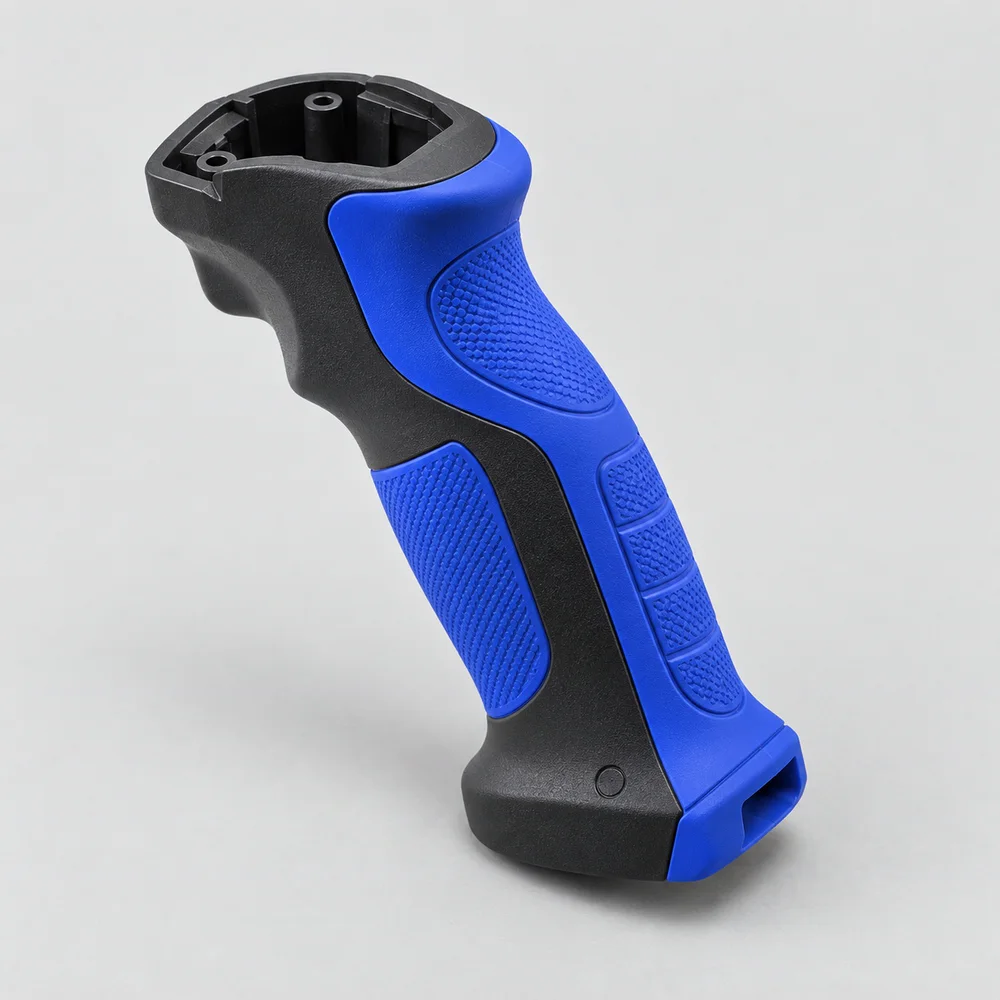
Overmolded power-tool grip, black nylon core with cobalt blue soft-touch TPE

Power-tool grip

Overmolded soft-touch over a rigid core

Material
PA66-GF + TPE
Volume
120k / yr
Tool
2-shot, 2 cav
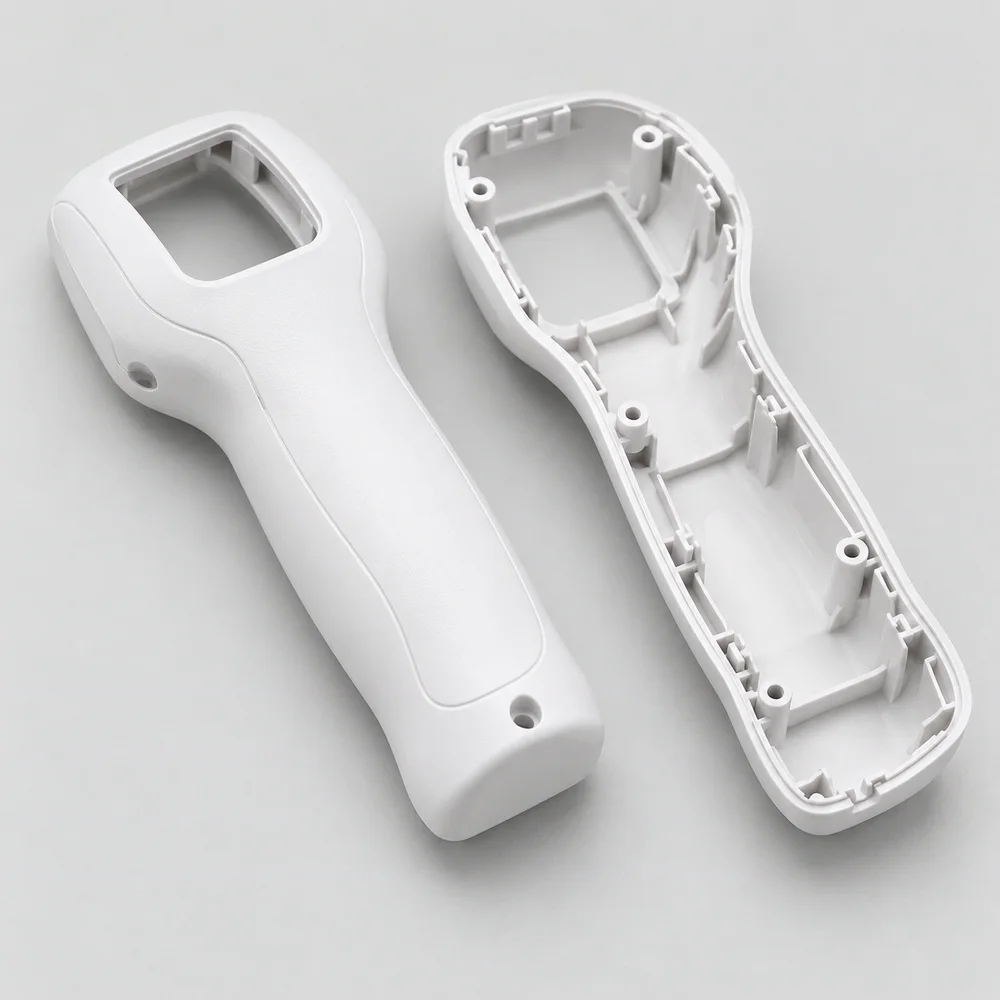
White medical device housing shells with internal ribs and screw bosses

Medical device housing

Molded in our ISO 13485 cleanroom cell

Material
PC/ABS
Volume
40k / yr
Tolerance
±0.05 mm
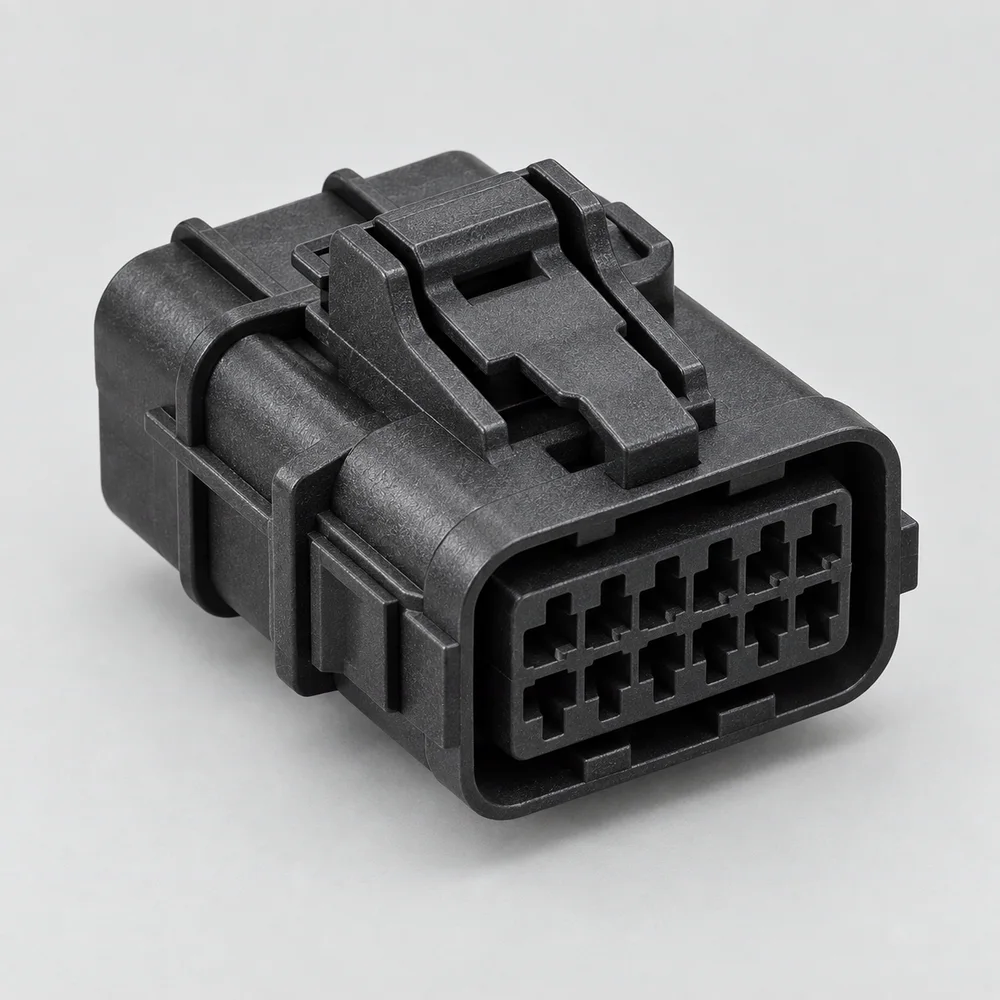
Black glass-filled nylon automotive connector housing

Connector housing

Fine pin cavities, locking latch

Material
PA66-GF30
Volume
2M / yr
Tool
16 cav, hot runner
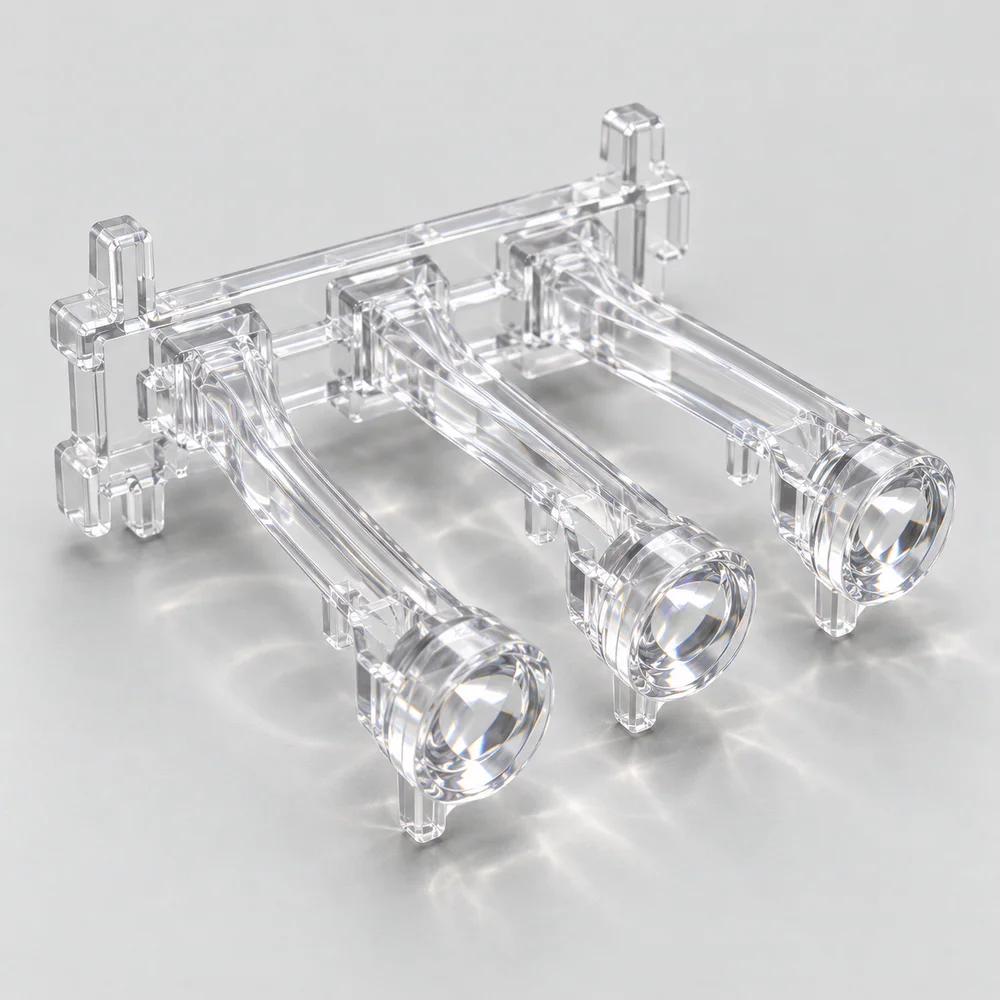
Crystal clear polycarbonate light pipe

Light pipe

Optically clear, mirror-polished tool

Material
Optical PC
Volume
250k / yr
Finish
SPI A-1
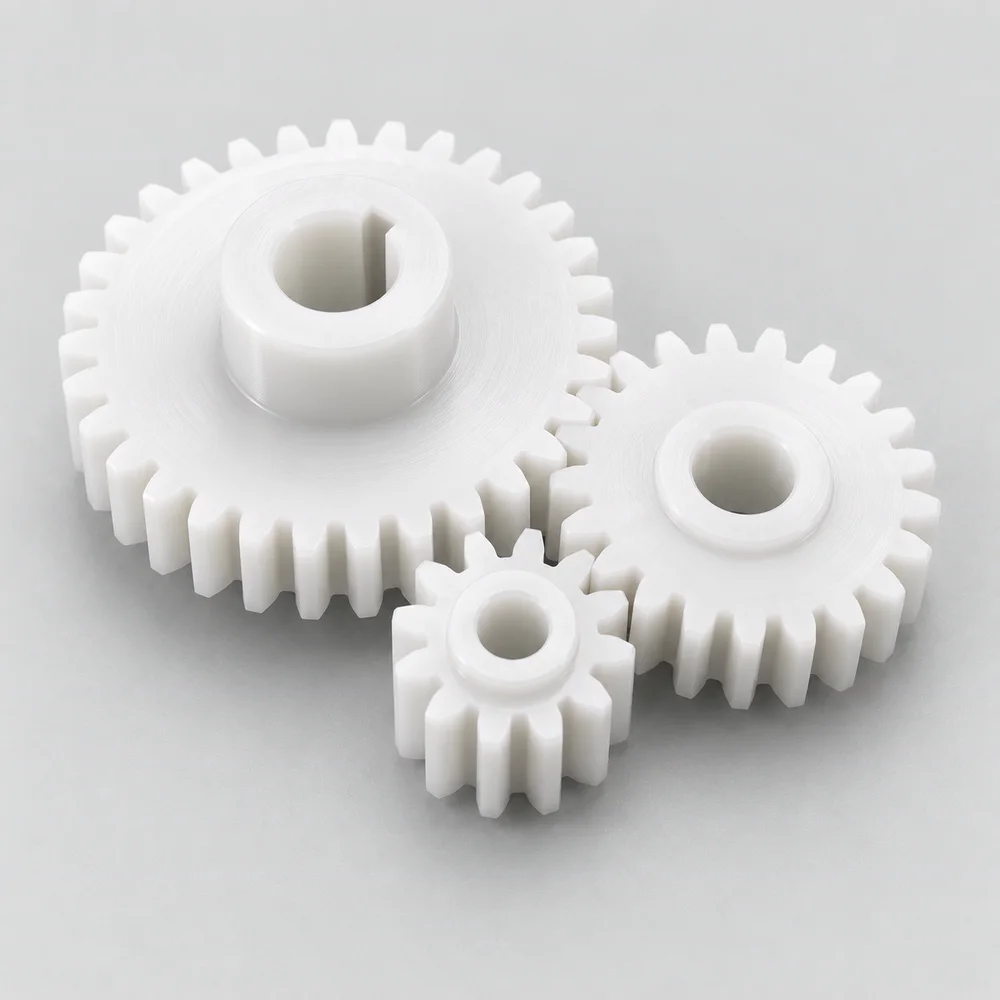
Set of white acetal gears

Gear set

Tight tooth profiles, low wear

Material
POM (acetal)
Volume
600k / yr
Tolerance
±0.02 mm
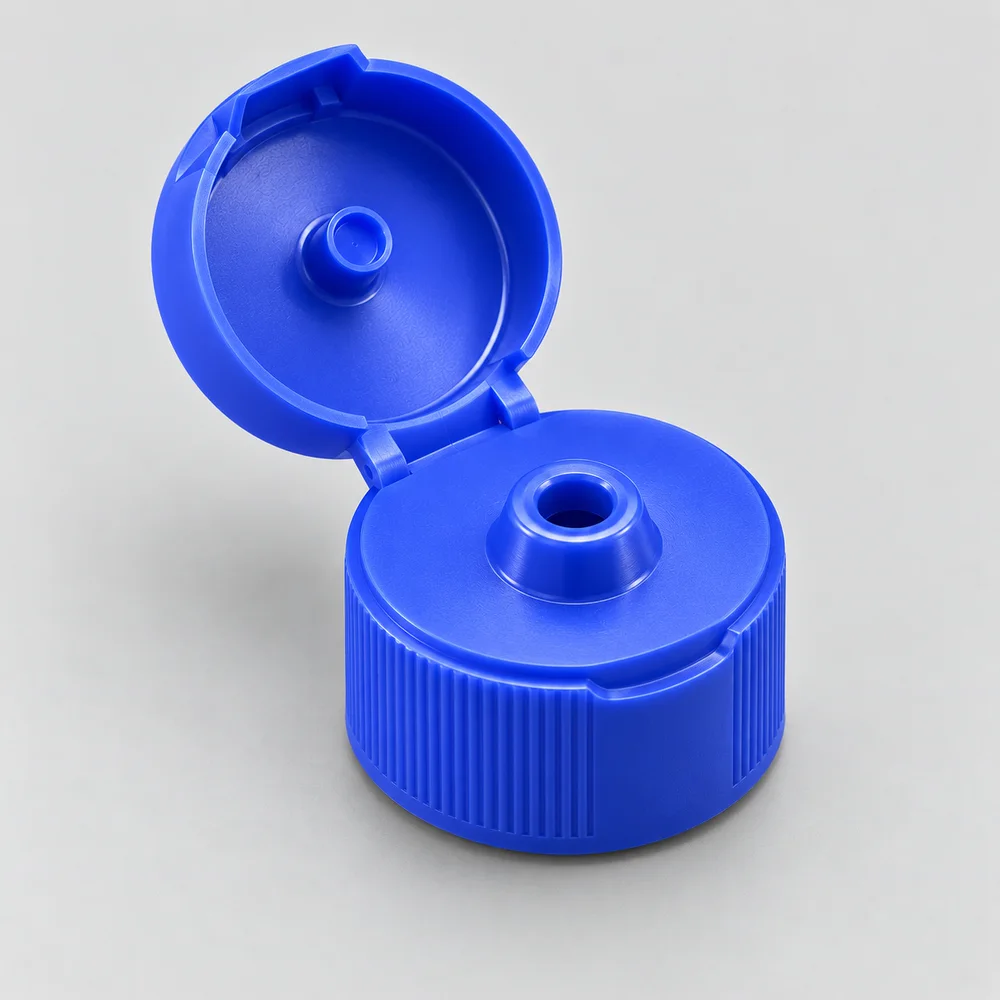
Flip-top dispensing closure with living hinge

Flip-top closure

Living hinge rated for 10,000 flips

Material
PP
Volume
5M / yr
Tool
32 cav, hot runner
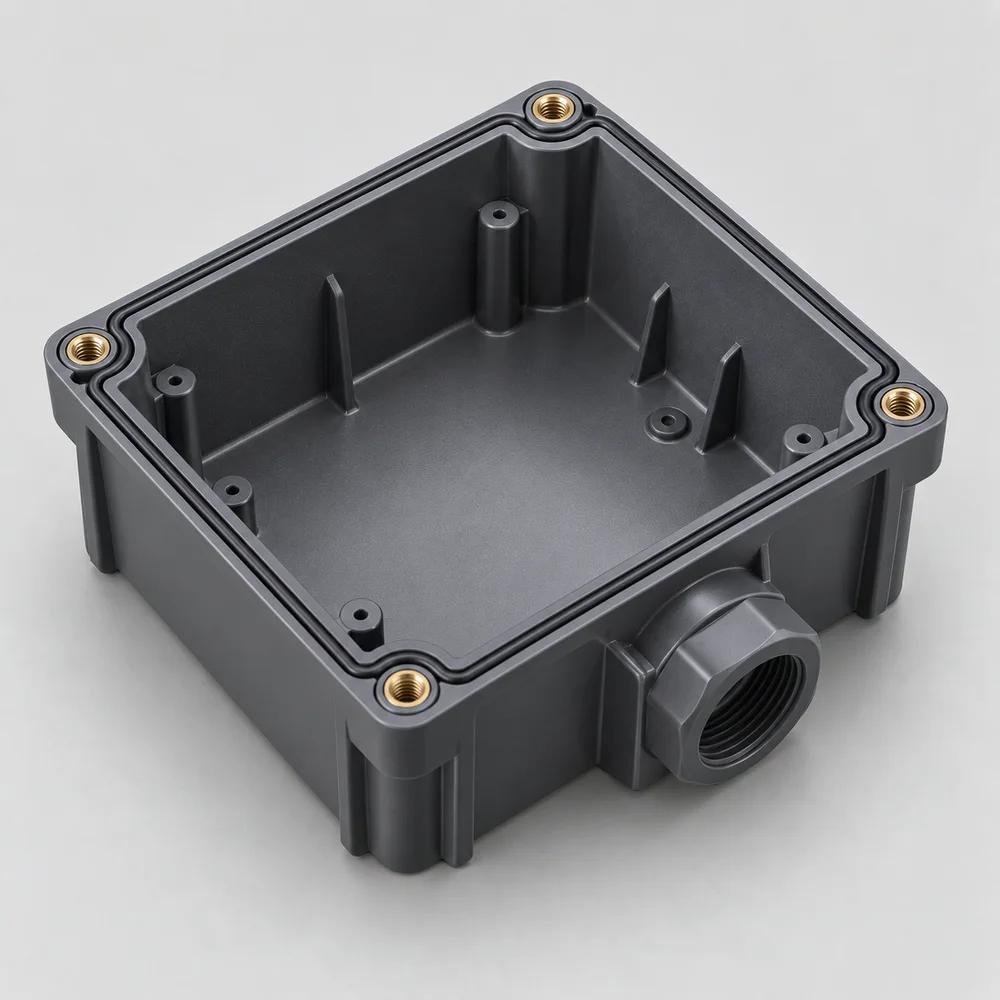
Grey polycarbonate IP67 electronics enclosure with gasket groove

IP67 enclosure

Gasket groove, brass inserts, UL 94 V-0

Material
PC, flame-rated
Volume
25k / yr
Extras
Inserts + seal
Yours next? Send us a drawing or a 3D file. Request a molding quote

04Common problems

Three problems buyers
bring us most.

Plain answers, and what we do about each one.

Problem 1

“Our parts warp, or measure differently every batch.”

Most of this is decided before production starts: where the plastic enters, how the mold cools, and whether the process is locked in. We fix it in the tool, then hold it on the press.

  • Gate and cooling layout simulated before we cut steel
  • Scientific molding: every press setting tested and written down
  • Pressure sensors inside the mold on critical parts
  • Critical dimensions charted every shift
Try it: move the gate
First to fillLast
Flow length
— mm
Weld lines
—
Warp risk
—

Drag the blue dot anywhere on the part.

Then we lock it in: wall thickness, last 60 partsCpk 1.67
2.05 mm2.00 nominal1.95 mm

Problem 2

“The tooling, or the price per part, is too high.”

Four things set your cost: how many you need, the plastic, the part design and the mold. Change one and the others move. Try it here.

  • More cavities cost more up front and less per part
  • Aluminum tools make short runs cheap
  • Small design changes can remove whole mold actions
  • We quote two tool options so you can compare
50010k100k1M2M
Plastic
Part size
Design
Mold we'd suggest

4-cavity steelBest total cost at this volume

Mold (one time)$38,000
Price per part$0.42
Per part, mold included, year one$1.18

Cost per part as volume grows→

Ballpark only. Your real quote comes from an engineer in 2 business days.

Problem 3

“We want to switch suppliers, but our mold is stuck there.”

Your mold can move. We inspect it, bring it over, sample it on our presses, and don't run production until you approve the parts.

  1. 1 · InspectA condition report with photos within 5 days of arrival.
  2. 2 · TransferWe arrange crating, freight, drawings and records.
  3. 3 · SampleFirst shots on our press, every critical dimension measured.
  4. 4 · ApproveYou sign off on the parts. Only then do we start production.
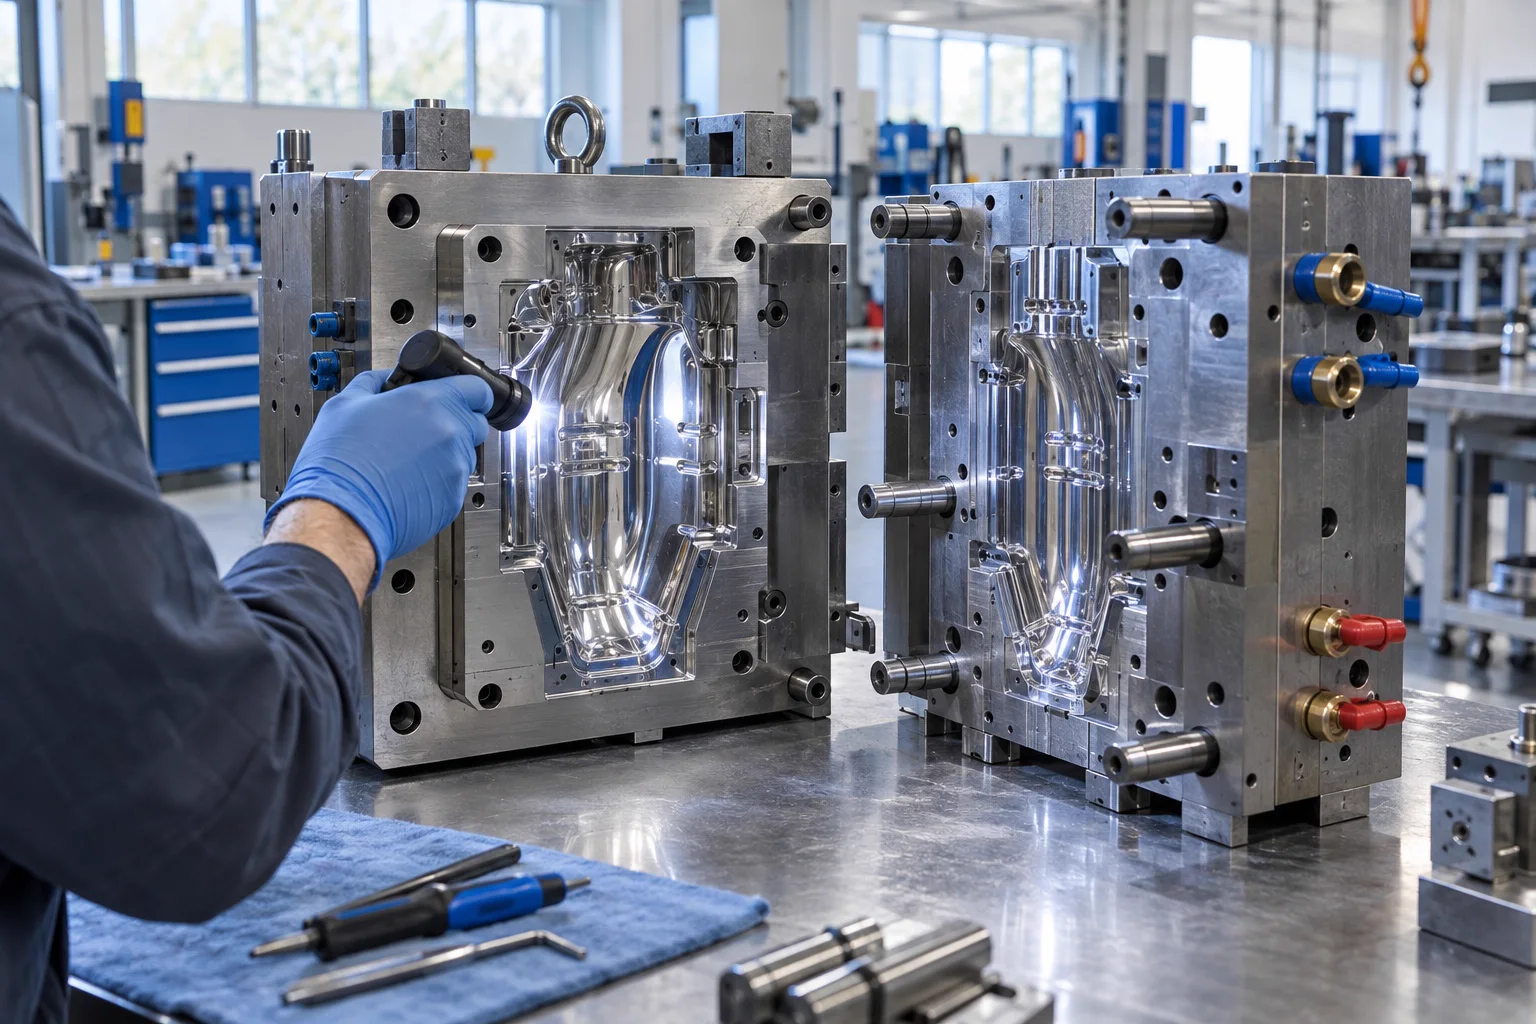
Toolmaker inspecting an open injection mold on a bench
Tool condition reportT-2291 · 8-cavity cap mold
Ready to sample
  • Parting line wearGood
  • Vents and gatesCleaned
  • Cooling flow, all circuits9.2 L/min
  • Ejector pins2 replaced
  • Hot runner, 8 zonesAll heating
  • Shot count to date1.8M
Inspected by R. Okafor, tool room leadDay 4 of 5

05Capabilities

The numbers
engineers ask for.

Everything on one sheet. Ask for the full equipment list.

Equipment capacity

38 presses

35 to 720 tons of clamp force, all-electric and hybrid, most with robot pick-off.

35–85 t8
110–220 t14
250–400 t9
450–720 t7
Part size

0.1 g to 2.5 kg

Parts up to 600 × 450 mm. Wall thickness 0.5 to 6 mm.

Production-volume fit

Best from 1,000 to 5M a year

Materials processed

60+ plastics

  • PPPolypropylene
  • ABSAcrylonitrile butadiene styrene
  • PCPolycarbonate
  • PA66-GFGlass-filled nylon
  • POMAcetal
  • PEEKPolyether ether ketone
  • TPEThermoplastic elastomer
  • PMMAAcrylic
  • PPSPolyphenylene sulfide
  • LSRLiquid silicone
  • HDPEHigh-density polyethylene
  • PBTPolybutylene terephthalate
Tooling capabilities

Built in our own tool room

  • Mold classesSPI 101–104
  • Cavities1 to 48
  • RunnersHot and cold
  • SteelsP20, H13, S136, aluminum 7075
  • ActionsSlides, lifters, unscrewing cores
  • Machines5-axis CNC, EDM, wire EDM
Surface finishes

Mirror to textured

Move your pointer over the samples.

SPI A-1Mirror
SPI B-2Semi-gloss
SPI C-1Matte
MT-11010Texture
Inspection methods
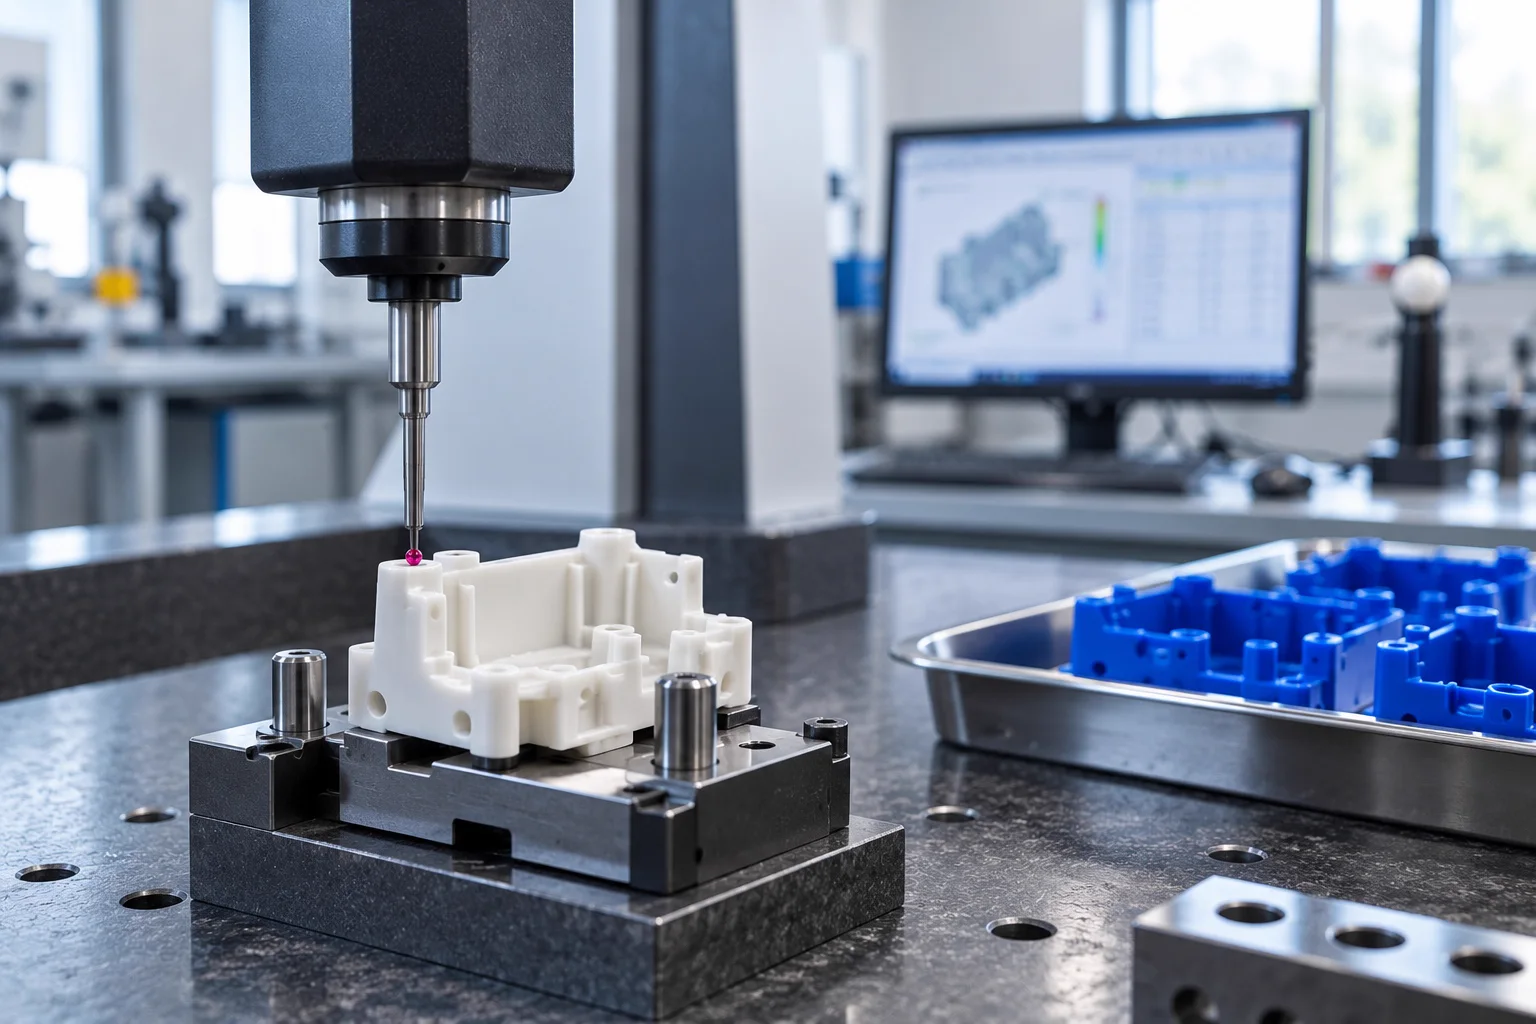
CMM probe measuring a molded plastic part
  • CMM
  • Vision systems
  • CT scanning
  • Optical comparator
  • First-article reports
  • PPAP
  • SPC, every shift
Secondary operations
  • Ultrasonic welding
  • Heat-set inserts
  • Pad printing
  • Laser marking
  • Heat staking
  • Assembly and kitting
  • Custom packaging

06Buyer questions

Questions buyers
ask first.

Short answers. Your engineer will cover the details on a call.

Is our quantity suitable?

If you need between 1,000 and 5 million parts a year, yes. Below that, a quick aluminum tool usually makes more sense, and we'll say so. If another process fits your part better, we'll tell you that too.

Can you use our existing mold?

Usually, yes. We inspect it first and send you a condition report with photos. If it needs repairs, you get a quote before we touch it. Most transfers have approved parts within 4 to 6 weeks.

Who owns and maintains the tooling?

You own the mold once it's paid for, and that's written into your quote. We maintain it at no extra cost: cleaning after every run, service at set shot counts, and a maintenance log you can see any time.

How do we approve samples?

We mold first samples, measure every critical dimension and send you parts plus the full report. You approve them, or we adjust the mold and send new samples. Production starts only after your sign-off.

How long does a new mold take?

Aluminum prototype tools take 2 to 3 weeks. Production steel takes 6 to 10 weeks. Your quote includes a week-by-week schedule.

07Start here

Send us your part.

An engineer, not a salesperson, reads every request. You get an answer in 2 business days.

  1. We review your filesDesign feedback included, even if you only asked for a price.
  2. You get a clear quoteMold cost, part price, lead time and who owns what.
  3. We walk through it togetherA 20-minute call with the engineer who reviewed it.
What helps us quote
  • Drawings or 3D files
  • Material
  • Quantities
  • Critical dimensions
  • Finish
  • Existing-tooling details
  • Delivery needs
Finish
Do you have a mold already?

Your files stay private. We sign NDAs before review if you ask.

Concept site by Figured Media. Not a real business.